Explore our top-rated B2B export inventory featuring precision-engineered thermal insulation, food-grade materials, and customizable OEM/ODM finishes.


Understanding user intent shifts, regulatory imperatives, and material innovations driving high-volume international sourcing from Chinese manufacturing hubs.
The global portable bottle and insulated drinkware market has evolved from simple utility containers into sophisticated lifestyle accessories, specialized outdoor equipment, and critical corporate sustainability channels. Valued at over $9.2 billion globally and expanding at a compound annual growth rate (CAGR) exceeding 6.4%, international procurement patterns reflect intense demand for high-performance thermal retention, zero-leak mechanics, and strictly certified food-safe material compositions.
For global buyers—spanning enterprise brand aggregators, outdoor sport outfitters, promotional item distributors, and private-label retail chains—navigating the manufacturing ecosystem in China requires rigorous evaluation of production automation, metallurgical grade consistency, regulatory compliance (FDA, LFGB, REACH), and custom OEM/ODM tooling capacity. China remains the unquestioned powerhouse of global drinkware manufacturing, accounting for over 75% of world production for double-wall stainless steel vacuum vessels.
Search intent mining across global commercial buyers demonstrates a decisive shift from low-cost sourcing toward value-density, ESG sustainability compliance, and technical customization. High-intent procurement queries prioritize suppliers capable of delivering:
A deep dive into metallurgy, insulation mechanics, and automated manufacturing processes engineered for longevity and food safety.
Utilizing premium Austenitic 18/8 Stainless Steel (SUS304) for inner and outer walls, alongside Surgical Grade 316 (SUS316) for extreme corrosion resistance against acidic beverages, coffee, and soup formulations.
Industrial high-vacuum annealing furnaces extract air between double walls to create near-absolute vacuum ($10^{-4}$ Torr), augmented by internal copper foil lining to reflect radiant heat energy back into the liquid core.
Lids and mouthpieces are crafted from virgin Tritan™ co-polyester, BPA-free Polypropylene (PP), and liquid food-grade silicone gaskets certified for thermal stability ranging from -40°C to +220°C without degassing.
| Material Category | Standard Specification | Thermal & Corrosion Threshold | Primary Industrial Applications |
|---|---|---|---|
| SUS304 (18/8 Food Grade) | 18% Cr, 8% Ni Composition | Up to 800°C oxidation resistance | Standard Travel Flasks, Daily Water Bottles, Sports Hydration |
| SUS316 (Surgical Grade) | 18% Cr, 10% Ni, 2% Mo | Superior acid/saline corrosion resistance | Infant Thermal Jars, Coffee Tumblers, Specialty Food Flasks |
| Tritan™ / Borosilicate Glass | BPA/BPS-Free Polymers / Thermal Glass | High transparency, -20°C to 120°C impact test | Clear Gym Bottles, Snowglobe DIY Tumblers, Lab Beakers |
| Food-Grade Silicone | Shore A 50-60 Durometer Gaskets | Permanent flexibility, non-porous seal | Collapsible Travel Bottles, Leak-proof Lid Seals, Straw Ports |
Excellence in custom OEM/ODM drinkware development, advanced automation, and global compliance.
Foshan Calmora Bottle Co., Ltd. is a professional manufacturer specializing in water bottles, tumblers, vacuum flasks, and food jars, offering comprehensive custom drinkware solutions for global markets. Located in Foshan, a major manufacturing hub in China, the company combines advanced production capabilities with efficient supply chain management to deliver high-quality and competitively priced products.
Founded in 2012, Calmora began as a small-scale producer of stainless steel bottles for domestic clients. By 2016, the company expanded its operations with automated production lines for double-wall vacuum insulation technology, entering overseas markets across North America and Europe. In 2020, Calmora further upgraded its R&D and design capabilities, enabling full OEM and ODM services, including custom branding, color finishing, and packaging solutions tailored to diverse customer needs.
The company’s product range includes insulated water bottles, travel tumblers, thermal vacuum flasks, and food jars designed for both everyday use and outdoor applications. With a strong focus on durability, safety, and performance, all products are manufactured using food-grade materials and strict quality control processes.
Foshan Calmora Bottle Co., Ltd. is certified with ISO 9001 quality management system and complies with international standards such as FDA and LFGB. Committed to innovation and sustainability, Calmora continues to provide reliable, eco-friendly drinkware solutions worldwide.
From custom rapid prototyping to automated mass assembly, providing complete OEM/ODM infrastructure for diverse global markets.
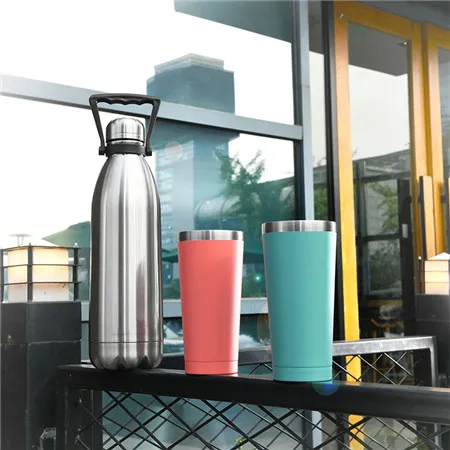
Designing ultra-rugged 32oz to 50oz wide-mouth hydro jugs with scratch-resistant powder coatings, heavy-duty handles, and high-impact protection bases tailored for hiking, camping, and fitness brands.
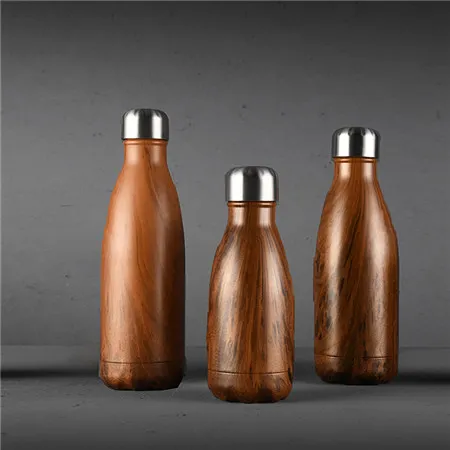
Tailor-made promotional executive gift sets with laser-etched branding, Pantone-matched electroplated hues, custom velvet-lined presentation boxes, and premium soft-touch exterior coatings.
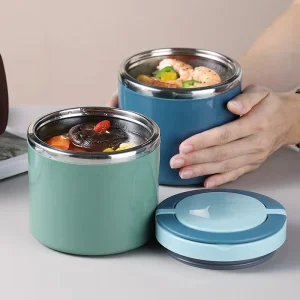
Wide-mouth insulated food jars featuring integrated foldable stainless steel spoons, pressure-release safety valves, and multi-tier insulated compartments for soup and meal warming on the go.
Calmora’s dedicated engineering hub accelerates project development times from raw initial CAD concepts to functional physical prototypes in as few as 7 to 10 working days. The full OEM/ODM execution matrix encompasses:
Protecting global brands through rigorous testing, full raw material traceability, and standardized quality assurance protocols.
Entering strict commercial markets in North America, Western Europe, Japan, and Australia requires full adherence to food-contact legislation, environmental mandates, and social accountability frameworks. Foshan Calmora Bottle Co., Ltd. operates under strict Quality Assurance (QA) and Quality Control (QC) frameworks from raw material intake to final outward delivery.
Pioneering smart temperature monitoring, eco-friendly materials, and ultra-lightweight structural engineering.
The next decade of drinkware innovation is defined by the convergence of micro-electronics, circular economy principles, and advanced metallurgical processing. Manufacturers leading the market are actively deploying solutions that integrate continuous user value with environmental stewardship.
Integration of low-power LED touch sensors, real-time liquid temperature readouts, and UV-C LED sterilization modules built directly inside caps to eliminate 99.99% of waterborne pathogens.
Transitioning toward 90% recycled post-consumer stainless steel (PCR SUS304) to drastically reduce carbon footprint, paired with plant-derived PLA and bio-based plastics for lids.
Utilizing high-precision wall-spinning technologies to reduce inner layer thickness down to 0.4mm while maintaining structural strength, reducing total bottle weight by over 30% for ultra-light outdoor usage.
Detailed answers to essential questions regarding B2B bulk orders, manufacturing customization, lead times, and quality assurance.
Our standard MOQ for custom color painting and screen-printed logos starts at 1,000 units per style/color. For fully customized bottle shapes or specialized tooling (ODM projects), MOQ ranges between 3,000 to 5,000 units depending on technical complexity and mold design requirements.
Every vacuum flask manufactured in our facility undergoes a 100% automated high-temperature infrared thermal inspection test after the vacuum sealing stage. Bottles that fail to meet thermal retention standards (e.g., maintaining liquids above 68°C after 6 hours) are automatically rejected by optical sensors.
Yes. We strictly utilize food-grade stainless steel (SUS304 or SUS316), BPA-free Tritan co-polyesters, and food-grade silicone. We provide complete testing reports from accredited third-party laboratories (SGS, TUV, Intertek) matching FDA 21 CFR and European LFGB compliance requirements upon request.
Sample customization with custom logos typically requires 7 to 10 days. Mass production lead time is generally 30 to 45 days after pre-production sample approval and deposit confirmation, depending on order size and complexity of custom packaging.
Absolutely. We offer comprehensive packaging solutions including custom color box printing, FSC certified Kraft boxes, inner protective sleeves, barcode labeling, FNSKU stickering, and direct palletization for Amazon FBA fulfillment centers worldwide.
Discover versatile sports hydration bottles, glass liquor containers, acrylic snowglobe tumblers, and high-capacity jugs.


 Calmora Bottle


